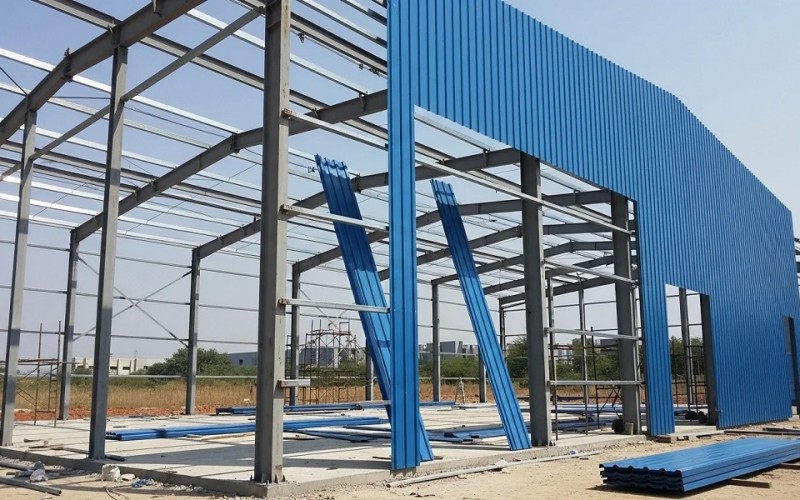
Pre-Engineered Building (PEB) Manufacturing is the off-site design, fabrication, and finishing of structural steel building components. Instead of fabricating materials on the construction site, each element such as primary frames, purlins, wall panels, and roof sheeting is precisely engineered and manufactured inside a controlled plant environment, then shipped to the job site for rapid bolted assembly.
Core Structural Components
Primary Framing Members: Heavy-duty load-bearing components, including built-up "I"-shaped tapered or uniform columns and rafters. These absorb major gravitational, seismic, and wind loads.
Secondary Members (Cold-Formed): Roof purlins, wall girts, and eave struts. Typically roll-formed into Z or C shapes to provide lateral support and anchor cladding panels.
Sheeting & Cladding: Pre-painted galvanized or Galvalume profile sheets and insulated sandwich panels (PUF/PIR/Rockwool) forming the outer roof and exterior walls.
Accessories & Bracing: Cable or rod cross-bracings, sag rods, anchor bolts, ridge ventilators, skylights, gutters, downspouts, and flashing trims.
End-to-End Manufacturing Process
1. Design & Detailing: Engineers calculate site-specific load conditions (wind speed, seismic zone, dead and live loads) to create optimized shop fabrication drawings, component nesting schedules, and bill of materials (BOM).
2. Plate Cutting & Edge Preparation: High-tensile steel plates (typically ASTM A572 Grade 50 or IS 2062) are cut to precision profile sizes using CNC plasma, oxy-fuel cutting torches, or multi-head beam slitters.
3. Fit-Up & Automatic Submerged Arc Welding (SAW):Flange and web plates are aligned in specialized H-beam assembly stations and continuously joined using automated Submerged Arc Welding (SAW) to produce built-up tapered frames.
4. Secondary Roll Forming & Punching: Galvanized steel coils undergo continuous cold roll-forming lines to produce high-tensile Z and C purlins, complete with pre-punched bolt holes at calculated intervals.
5. Surface Treatment & Protective Coating: Fabricated members undergo abrasive shot/grit blasting (typically to SA 2.5 standards) to strip rust and scale, followed immediately by anti-corrosive primer and topcoat industrial epoxy or polyurethane paint.
6. Quality Inspection & Bundling: Components undergo rigorous dimensional checks, ultrasonic or non-destructive weld testing (NDT), dry film thickness (DFT) paint verification, and barcode tagging for phased site delivery.